|
Product Details:
|
| Purification Light: | More Than 300Lux | Hepa Filter Efficiency: | 99.999% @0.3um |
|---|---|---|---|
| Keywords: | Cleanliness | Cleaness Level: | ISO 5/ISO6/ISO7/ISO8 |
| Fireresistance: | Complies With Fire Safety Standards | Window: | Double-layer Vacuum Organic Glass |
| Size: | Customized | Noise Level: | ≤65dB |
| HEPA Efficiency: | 99.999% @0.3μm | Cleanliness Level: | ISO 5/6/7/8 |
| Illuminance: | >300 Lux | Window Material: | Double-layer Vacuum Organic Glass |
| Flooring Options: | Raised Flooring / Anti-static Flooring | ||
| Highlight: | Raised Flooring Modular Cleanroom,Double-layer Vacuum Organic Glass Cleanroom System,ISO 5 to ISO 8 Cleanliness Cleanroom System |
||
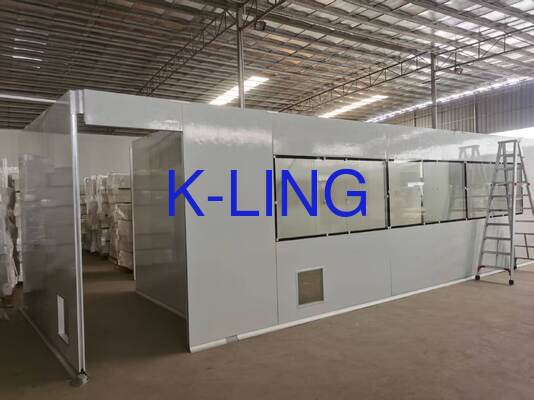
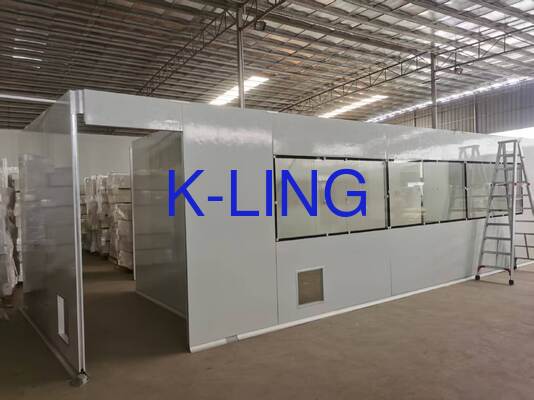
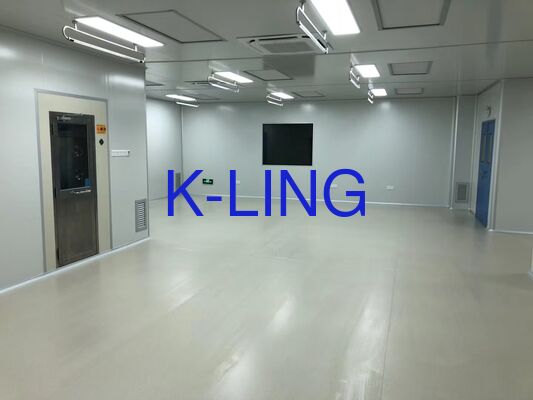
The Modular Cleanroom is a state-of-the-art solution engineered to meet the rigorous demands of controlled environments across multiple industries. Its innovative modular design delivers exceptional flexibility and efficiency, making it an ideal choice for organizations seeking a reliable and customizable cleanroom system. Whether you require a Movable Cleanroom for temporary setups, an ISO 6 Cleanroom for stringent contamination control, or a Detachable Cleanroom for easy reconfiguration, this system adapts to every need with consistent performance and convenience.
A defining feature of the Modular Cleanroom is its customizable size. Recognizing that every application has unique spatial requirements, the cleanroom can be tailored to specific dimensions, ensuring optimal use of available space. From compact units for small-scale operations to expansive configurations for large production lines, the modular design integrates seamlessly with your project specifications.
The Modular Cleanroom offers two flooring configurations, both engineered to enhance functionality and safety:
Fire safety is a critical consideration in any cleanroom environment, and the Modular Cleanroom fully complies with fire safety standards. The materials and construction methods employed ensure enhanced fire resistance, safeguarding personnel and valuable equipment against potential fire hazards. This compliance not only meets regulatory requirements but also reflects a commitment to creating a secure and resilient workspace.
Maintaining superior air quality is central to the cleanroom's functionality. Equipped with HEPA filters boasting an efficiency of 99.999% at 0.3 microns, the Modular Cleanroom effectively removes particulate contaminants from the air. This level of filtration ensures that airborne particles — including dust, bacteria, and other microscopic impurities — are minimized to meet the stringent cleanliness criteria of an ISO 6 Cleanroom environment. Such high-efficiency filtration is vital for industries such as pharmaceutical, biotechnology, electronic, and healthcare, where contamination control is paramount.
In addition to its advanced filtration capabilities, the cleanroom features purification lighting that delivers illumination exceeding 300 Lux. This lighting standard provides bright, uniform visibility essential for precision tasks while minimizing heat generation and reducing the risk of contaminant accumulation. The thoughtful integration of purification lighting enhances both operational efficiency and environmental hygiene within the cleanroom.
The Modular Cleanroom's design emphasizes mobility and ease of assembly, making it an excellent choice for enterprises requiring a Movable Cleanroom solution. Detachable panels and components allow for quick installation, dismantling, and relocation without compromising structural integrity or cleanliness standards. This versatility supports dynamic operational needs, enabling rapid adaptation to changing workflows or spatial configurations.
Overall, the Modular Cleanroom stands out as a highly adaptable, safe, and efficient cleanroom system. Its combination of customizable sizing, advanced flooring options, stringent fire resistance, superior HEPA filtration, and optimal illumination makes it a comprehensive solution for a wide range of cleanroom applications.
| Product Name | Modular Cleanroom (Hardwall / Softwall Cleanroom) |
|---|---|
| Compliance Standards | Meets GMP, FDA, ISO Cleanroom Standards (ISO 7 cleanroom) |
| Noise Level | ≤65 dB |
| Fire Resistance | Complies with fire safety standards |
| Window | Double-layer vacuum organic glass |
| Size | Customized |
| HVAC System | Compliant |
| Purification Light | More than 300 Lux |
| Lighting | Integrated LED lighting |
| Additional Features | Integration Modular Cleanroom with Laminar Flow Booth |
The K-Ling Modular Cleanroom, model number KEL-LFB, is an advanced ISO 6 modular cleanroom solution designed to meet the highest standards of cleanliness and purification. Originating from China and certified with CE, this cleanroom system is ideal for industries requiring controlled environments, including pharmaceutical, biotechnology, electronics manufacturing, food processing, and research laboratories. Its modular design allows for rapid assembly and easy scalability, making it perfect for projects that demand flexibility and customization in size and layout.
K-Ling offers a reliable supply ability of up to 5000 square meters per month, coupled with a delivery time of only 15 working days after receipt of deposit, facilitating quick project turnaround times. Payment terms are flexible, accepting TT or LC to accommodate diverse business requirements. This modular cleanroom product is an excellent choice for companies seeking a high-quality, customizable, and efficient cleanroom solution that maintains strict cleanliness and environmental control standards.
In summary, the KEL-LFB Modular Cleanroom by K-Ling is ideal for cleanroom applications where cleanliness, flexibility, and rapid deployment are critical. Whether you need a small detachable cleanroom for specialized tasks or a large integration modular cleanroom for complex operations, this product provides a dependable and scalable solution tailored to your specific needs.
Contact Person: Mrs. Zhao
Tel: 86 20 13378693703
Fax: 86-20-31213735