Product Overview
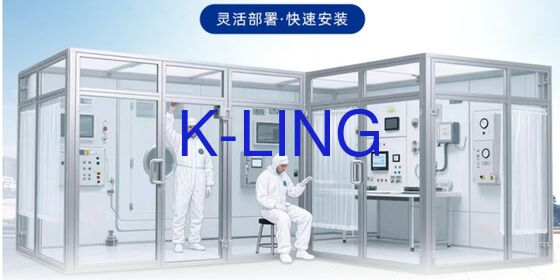
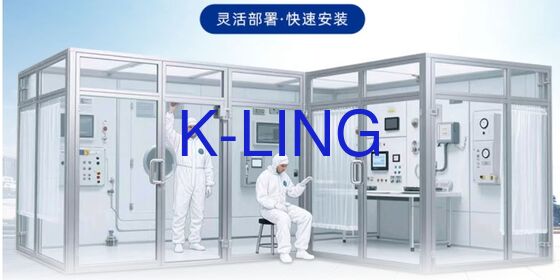
The Modular Cleanroom is an advanced, high-quality cleanroom solution engineered to meet the stringent requirements of modern industries. Built with precision and flexibility in mind, it provides an ideal environment for applications that demand controlled contamination levels and superior air quality. The system is designed to comply with critical cleanliness standards including GMP, FDA, and ISO Cleanroom Standards, making it a reliable choice for pharmaceutical, biotechnology, electronics, and semiconductor manufacturing, among other sectors.
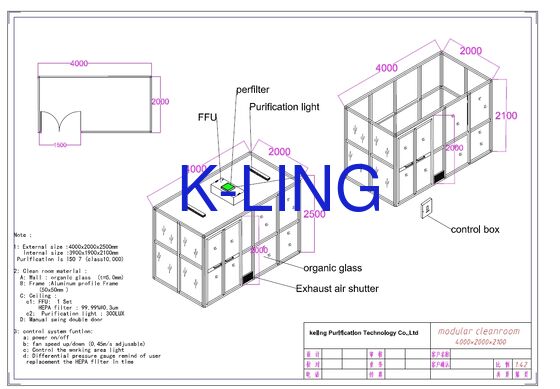
A standout feature is its adherence to ISO7 Cleanroom classification, ensuring the environment maintains a low particle count and meets rigorous cleanliness specifications. This level of control is essential for processes where even the smallest contaminants can compromise product quality and safety. The cleanroom's design supports consistent air quality and pressure differentials, helping maintain the integrity of sensitive operations.
The Modular Cleanroom is also recognized for its noise efficiency, operating at ≤65dB. This low noise output ensures a comfortable working environment for personnel, reducing fatigue and enhancing productivity during extended periods of operation — a significant advantage in settings where concentration and precision are paramount.
Incorporating a high-performance HVAC system that complies with industry standards, the cleanroom guarantees optimal air filtration, temperature, and humidity control. The HVAC system is engineered to provide a stable and contaminant-free atmosphere, which is crucial for maintaining the cleanliness class and protecting both products and personnel. It supports effective airflow patterns and filtration mechanisms that reduce particulate matter and microbial contamination.
The cleanroom's double-layer vacuum organic glass windows are another key feature, offering excellent visibility while maintaining airtightness and insulation. These windows provide clear sightlines into the cleanroom without compromising the controlled environment, allowing for easy monitoring and supervision. The double-layer construction enhances durability and thermal efficiency, contributing to the overall stability of the cleanroom conditions.
Designed with modularity and mobility in mind, the Modular Cleanroom offers unparalleled flexibility. It can be easily assembled, disassembled, and relocated as needed, making it an excellent choice for businesses that require adaptable cleanroom solutions. Whether expanding production lines or shifting operations, the movable design facilitates quick adjustments without extensive downtime or costly renovations.
Furthermore, the modular construction enables customization to fit specific spatial requirements and operational needs. This adaptability allows organizations to optimize their cleanroom footprint, ensuring maximum efficiency and cost-effectiveness. The cleanroom panels and components are fabricated with high-quality materials that resist corrosion, wear, and contamination, ensuring longevity and easy maintenance.
Overall, the Modular Cleanroom combines compliance, comfort, and convenience in one comprehensive system. Its compliance with GMP, FDA, and ISO standards guarantees that it meets the highest industry benchmarks for cleanliness and safety. The low noise level, efficient HVAC system, and durable double-layer vacuum organic glass windows enhance the user experience and operational reliability. Additionally, its modular and movable design offers businesses a versatile solution that can evolve alongside their needs.
Applications
The K-Ling KEL-LFB modular cleanroom is an advanced prefabricated cleanroom solution designed to meet the stringent requirements of modern industries. Originating from China and certified with CE, this Class 1000 modular cleanroom ensures a dust-free cleanroom environment, crucial for sectors demanding high levels of contamination control. Its design complies with GMP, FDA, and ISO cleanroom standards, making it ideal for pharmaceutical manufacturing, biotechnology labs, electronics assembly, and food processing facilities.
Pharmaceutical Production
One of the key application occasions for the K-Ling KEL-LFB is pharmaceutical production, where maintaining a dust-free cleanroom is essential to prevent contamination and ensure product safety. The modular nature allows for rapid installation and scalability, accommodating various production scales from small laboratories to large manufacturing floors. The integrated LED lighting provides more than 300Lux of purification light, enhancing visibility and operational efficiency within the cleanroom environment.
Electronics Manufacturing
In the electronics industry, the Class 1000 modular cleanroom plays a vital role in protecting sensitive components from particulate contamination. The raised or anti-static flooring options available with the K-Ling KEL-LFB model contribute to static control and ergonomic workspace design, reducing the risk of electrostatic discharge that could damage delicate electronics. Additionally, the cleanroom's fire resistance compliance ensures workplace safety, meeting fire safety standards required in high-tech manufacturing settings.
Research Laboratories & Medical Devices
The prefabricated cleanroom is also highly suitable for research laboratories and medical device production, where precision and cleanliness are paramount. Its packaging with POLYWOOD ensures safe transportation, and with a supply ability of 5000SQM per month, K-Ling can reliably meet high demand. Customers benefit from flexible payment terms such as TT/LC and a delivery time of just 15 working days after deposit, making the KEL-LFB model an efficient and cost-effective cleanroom solution priced between 800–5000SQM.
Overall, the K-Ling KEL-LFB modular cleanroom provides a versatile, compliant, and easy-to-install environment that supports critical processes requiring a dust-free cleanroom. Whether for pharmaceutical, electronics, or medical applications, this prefabricated cleanroom ensures optimal conditions aligned with the highest industry standards.

 Your message must be between 20-3,000 characters!
 English